If you’ve been diving into solar tech lately, you’ve probably heard “N-Type TOPCon” thrown around like it’s the new shiny upgrade for panels. And as someone who’s been in the game as an N-Type TOPCon solar panels supplier for the last 6 years, I can tell you—this tech isn’t just hype. It’s way more efficient, more durable, and actually solves a lot of the problems that old P-Type panels have. But if you’re wondering what makes these panels tick under the hood? It all starts with the raw materials. Let’s break this down in plain talk, no overly science-y jargon that’ll make your head spin. N-Type TOPCon Solar Panels
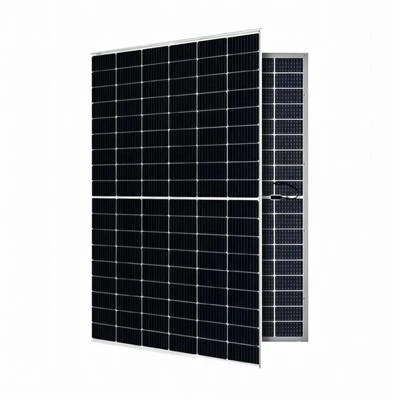
First off, let’s get one thing straight: N-Type TOPCon’s core is all about silicon, but it’s not your run-of-the-mill silicon that went into panels 10 years ago. P-Type panels (the older ones) used what’s called “Boron-doped” silicon, but N-Type flips that—we use “Phosphorus-doped” silicon instead. That’s a big reason why they perform better in low light, right? But not just any N-Type silicon will do. We’re talking about monocrystalline silicon wafers here, specifically the high-purity kind—99.9999% pure, to be exact. Yeah, that’s six nines.
Wait, let me explain that simple: Silicon comes from sand, but to get to that 99.9999% level, you have to melt it down, purify it over and over again, and pull it into long, thin ingots. Then you slice those ingots into super thin wafers—usually 150 to 180 microns thick, which is way thinner than a human hair. Why monocrystalline, not polycrystalline? Because monocrystalline has a single, continuous crystal structure. That means fewer defects, less energy lost as the sun’s light hits it, and overall higher efficiency. For TOPCon, we use what’s called “n-type monocrystalline Cz silicon” (Cz stands for Czochralski, the process for making those ingots) — it’s the gold standard right now because it’s consistent and gives us that stable base we need for the TOPCon layer. I’ve sourced these wafers from a few trusted partners, and the difference in performance is night and day compared to poly stuff.
Next, the secret sauce of TOPCon itself—wait, what does TOPCon stand for? Tunnel Oxide Passivated Contact. Yeah, it’s a mouthful, but the two key parts here are the tunnel oxide layer and the polysilicon layer that goes on top of it. Let’s start with the tunnel oxide. That’s a super thin layer of silicon dioxide—like, only 1 to 2 nanometers thick. That’s so thin you can barely see it, but it does two huge things: it stops charge carriers (the electrons that make electricity) from leaking out of the panel, and it lets enough electrons pass through from the silicon wafer to the conductive layer above it. For this oxide, we use ultra-pure oxygen, usually from high-quality industrial gases. No impurities here—even a tiny bit of metal or moisture would mess up that thin layer and kill efficiency. I remember a batch we messed up early on because we used cheaper oxygen, and the panels had 2% lower output than expected. Lesson learned: this stuff matters.
Then right on top of that tunnel oxide is the doped polysilicon layer. This is another thin layer—around 50 to 100 nanometers thick, so still super thin—but it’s doped with phosphorus too, just like the base wafer. That’s what makes the contact work perfectly, no extra energy lost. Polysilicon here isn’t the same as the poly wafers I mentioned earlier. This is ultra-thin, high-purity polysilicon deposited via a process called LPCVD (Low-Pressure Chemical Vapor Deposition)—but I won’t bore you with the process, just know it’s made from silane gas and dopants, and it’s all about being as defect-free as possible. If this layer has even a tiny hole, electrons leak out, and your panel’s efficiency drops. We test every single wafer for pinholes before we even move to the next step—no cutting corners here.
Now, we can’t forget the metal contacts. Even if you have the perfect silicon and TOPCon layers, you need something to carry that electricity out of the panel and into your home or grid. For N-Type TOPCon, we use silver, but not just any silver. Wait, people used to use aluminum for contacts, but silver is way more conductive—so it’s the go-to now. But here’s the thing: we’re using “silver pastes” that are optimized for N-Type wafers. Old silver pastes for P-Type panels don’t work as well on N-Type because they can cause extra contact resistance. Our suppliers make special silver pastes with smaller particles, so they can print thinner lines on the wafer (less silver used, which actually saves costs without hurting performance). Also, we use a “front-side” and “back-side” contact—front side is the grid lines that catch sunlight, so they have to be thin enough to not block light, but thick enough to carry current. Back side is a full layer, so no gaps there. I’ve had customers ask if we can cut silver to lower costs, but that’s a big no—silver is the most expensive part after silicon, but skimping here leads to panel failure in a few years. We do use a tiny bit of copper in some pastes for back contacts now, to reduce silver use, but it’s controlled so it doesn’t cause corrosion.
Another material you don’t see, but is 100% necessary: the anti-reflective (AR) coating. That’s the thin blue (or sometimes black) layer on the front of the panel. Its job is simple—stop sunlight from bouncing off the silicon wafer before it can turn into electricity. For TOPCon, we use a dual-layer AR coating, usually made of silicon nitride or silicon oxide, sometimes with a layer of aluminum oxide. The thickness is super precise—like, we calibrate it to within a nanometer. If it’s too thin, it doesn’t block enough reflection; too thick, it blocks too much light. We tested a one-layer coating once, and the panels had 1.5% lower output—small number, but over 25 years, that’s a lot of lost energy for a customer.
Then we get to the encapsulants and the backsheet. These are the layers that protect the fragile solar cells from the elements—rain, UV light, wind, temperature changes. The encapsulant is usually EVA (ethylene vinyl acetate) or POE (polyolefin elastomer). POE is newer, and better for N-Type because it’s more resistant to UV degradation, which is a big deal since N-Type panels are more sensitive to long-term UV exposure. The backsheet is the layer on the back of the panel—we use ones with three layers: a weather-resistant outer layer, a core layer for insulation, and an inner layer that bonds to the encapsulant. No cheap backsheets here—we’ve had customers come to us with panels from other suppliers that failed after 3 years because the backsheet cracked. Ours are rated for 25 years minimum, so these materials have to hold up.
Wait, let’s not ignore the frame! Most N-Type TOPCon panels come with an aluminum frame. It’s lightweight, strong, corrosion-resistant, and easy to install. Aluminum is perfect because it doesn’t rust, and it’s easy to bend into the standard sizes we use (like 60-cell or 72-cell panels). We powder-coat the frames too, so they match the panel color and hold up to salt air if someone’s installing near the ocean. I’ve had a few projects where we used stainless steel frames for harsh coastal environments, but aluminum is the standard because it’s cheaper and works great for most places.
Now, let’s talk about why this matters for you, whether you’re a homeowner looking to switch to solar or a business owner scaling up. N-Type TOPCon isn’t just a better tech—it’s built with better raw materials, all chosen to fix the flaws of old panels. I see a lot of suppliers cutting corners on materials to undercut prices, but that’s a short-term win that hurts customers long-term. As someone who’s been in this space, I stand by every material we use—we source from partners that have been in the solar game for decades, no fly-by-night suppliers.
Let me wrap this up: the main raw materials for N-Type TOPCon panels are high-purity monocrystalline silicon wafers, the specialized tunnel oxide and polysilicon TOPCon layers, optimized silver (and copper) metal contacts, precision anti-reflective coatings, durable encapsulants and backsheets, and corrosion-resistant aluminum frames. Each part has to work in sync, and if any one material is off, the whole panel suffers.

If you’re looking for reliable N-Type TOPCon solar panels that are built to last and perform, we’ve got you covered. We’ve installed panels for residential and commercial projects across the country, and our customers consistently report higher energy output even in shaded or low-light areas. If you want to chat about your project, ask more about materials, or get a quote, don’t hesitate to reach out—we’re here to help you make the best choice for your solar needs.
Solar Panels References:
- Green, M. A., et al. (2020). Solar Cell Efficiency Tables (Version 55). Progress in Photovoltaics: Research and Applications.
- International Energy Agency (IEA) PV Technology Roadmap. (2021). Solar photovoltaic energy for a sustainable future.
- Fang, X., et al. (2019). Tunnel Oxide Passivated Contact (TOPCon) Solar Cells: A Review. Energy & Environmental Science.
- Silver Institute. (2022). Silver Demand for Photovoltaics: Trends and Outlook.
- Solar Energy Industries Association (SEIA). (2023). N-Type Solar Panel Technology: Market Status and Growth Projections.
Dongguan MylAn International Trade Co., Ltd.
As one of the most professional n-type topcon solar panels manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy advanced n-type topcon solar panels in stock here from our factory. Welcome to contact us for pricelist.
Address: Room 401, Building 5, No.7, Machong Section, Shuixiang Avenue, Machong Town, Dongguan City, Guangdong Province
E-mail: salee@mylansolar.com
WebSite: https://www.mylansolar.com/
