Hey everyone, it’s Jake here, and I run a gantry welding robot supply business that’s been around for over a decade. If you’re reading this, you’ve probably already invested in one (or are thinking about it) – and let’s be real, buying the robot is only half the battle. The other half? Training your workers to actually operate it without turning it into a $10k paperweight or, worse, a safety hazard. I’ve seen so many shops skip this step, and it always ends in frustration: delayed projects, wasted materials, and even some burnt wiring that made us cross our fingers and charge extra for emergency fixes. Today, I’m breaking down exactly how I train teams to get the most out of their gantry welding robots, no stuffy textbooks required. Gantry Welding Robots
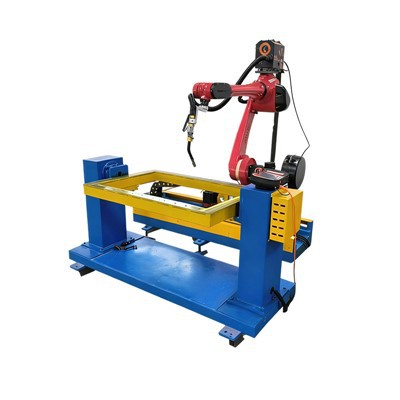
First off, let’s get one thing straight: your workers aren’t “tech newbies” just because they’re moving from manual welding. Most of the guys and gals I work with have 5+ years holding a welding torch, can read blueprints like their favorite recipe book, and know how to fix a mill when it acts up. The gap isn’t their skill – it’s rethinking how to apply that skill to a robot that moves at 500 inches a minute instead of their steady hand. When I start training, I never call anyone “trainees” – that term makes people check out. I say “operators-in-training” or, better yet, just “the team” – they’re already experts at what they do; we’re just adding a new tool to their belt.
The first step I always do is a 1-hour “no robot” intro, and I swear by this. No, you don’t need to wheel the 2,000-pound gantry unit out on day one. We grab a whiteboard, their old welding logs, and walk through what actually makes a good weld. I ask them to draw out the weld path they’d do manually on a steel beam – all the curves, the stop points for thick material, the spot where they need to slow down to avoid burn-through. Then, I draw how the robot sees that same path. That’s a lightbulb moment right there. Operators don’t realize gantry robots don’t “feel” the metal like they do – they just follow coordinates. So if their manual path has a tiny dip to compensate for a warped beam, the robot will miss it unless we program that in. This isn’t teaching them to weld all over again; it’s translating their hand skills to a machine’s language. I also use a cheap plastic gantry demo kit (we sell these for $50 as a side thing, no big markups) so they can move the axis sticks around and get a feel for how fast it moves – no risk of burning anything, just playing.
Next, hands-on time with a “dummy run” setup. This is non-negotiable for me. We grab scrap steel, a cheap MIG wire spool, and set up the robot in a fenced-off area (safety first, always). The first week, they don’t even strike an arc. I have them program the path using the robot’s teach pendant – that’s the big control screen, right? But I don’t let them touch the “run” button until they’ve walked through every step: setting the wire feed speed, the travel speed, the stickout distance. Wait, stickout is huge. Manual welders hold the torch at ½ inch, but with gantry robots, if it’s ¼ inch too long, the wire will wrap around the contact tip and jam the torch. I make them practice measuring it with a caliper every time – I even have a little sticker on the teach pendant that says “CHECK STICKOUT” in bold red. For the dummy runs, we use a neon pen that makes a bright line, so when the robot moves, they can see exactly where it’s going. If it’s off, they adjust the coordinates, no sparks, no waste. I usually run this for 3 days, 2 hours a day, and by then, they’re not scared of the teach pendant anymore – they’re annoyed when it doesn’t get the path right, same as they’d be with their own hand.
Once they’re confident with the dummy runs, we move to actual scrap metal welds, but with a strict “stop on error” rule. Here’s the thing: when the robot does mess up, I don’t fix it. I make them go back, watch the weld bead, and figure out why it’s lumpy or has gaps. Last month, a team in Detroit had a robot weld a 10-foot beam that had tiny rust spots, and the robot skipped those spots. The operator thought the program was wrong, but when we checked, the rust made the arc start delay longer than the robot’s path pause. So they adjusted the arc start time in the settings, and boom – perfect weld. That’s way better than me telling them what to do; they learn to problem-solve on their own, which is what you need when you’re welding production runs. I also have a “mistake log” that the team keeps – every time they mess up, they write it down, what went wrong, and how they fixed it. We review this for 10 minutes every Friday, and before you know it, they’re fixing issues I didn’t even know were possible.
Now, safety is not an afterthought – it’s the first rule, and I don’t cut corners here. Gantry welding robots are big, fast, and if you stick your hand in the wrong place, they’ll hurt you. I make everyone go through OSHA’s robotic safety course (but I condense it to 2 hours, because who has time for a 8-hour course?) and then we do hands-on safety drills. For example, we tape a “safety fence” around the robot, and practice what happens if you open the gate while it’s running – the robot stops instantly. I also have each operator practice an emergency stop 10 times, from all different angles. The first time I trained a team in Texas, the new operator tried to reach for something while the robot was moving, and they hit the emergency stop before I even said anything. That’s the win right there. I also stress that no one works alone with the robot – even the night shift has two people, one running the teach pendant, one watching for issues. It’s not paranoia; it’s how you keep everyone whole.
Wait, let’s talk about customizing the training for your shop, not just mine. Every welding job is different – some shops weld thick steel for bridges, some do thin parts for trailers, some work on small frames for machinery. One size doesn’t fit all, and I refuse to run a generic training program. When a shop in Florida does mostly aluminum welds, I skip the steel dummy runs and use aluminum scrap, teach them about gas settings specifically for aluminum, and practice path adjustments for thin metal that burns through easy. For a shop that does long gantry runs (like 50-foot beams), we do extra practice with axis syncing – that’s when the gantry moves along X, Y, and Z at the same time without warping the weld. I bring in actual project parts that they’ll be welding, so they’re training on the exact stuff they’ll make every day. That way, when they go live, it’s not a big unknown – it’s just another day at work.
I also keep a open line post-training, because training doesn’t end when you leave the shop. I work with every team for 30 days after the initial training, via video calls or on-site visits, to fix kinks. Last quarter, a team in Chicago was having trouble with the robot’s wire feed skipping, so I hopped on a Zoom call, had them show me the robot’s settings, and we realized they were using a wire spool that wasn’t tensioned right – easy fix, but I would’ve never known if I didn’t check in. And I tell everyone: if you’re stuck at 2 a.m. and the robot’s throwing an error, shoot me a text (no, I don’t answer at 2 a.m., but I get it in the morning). This isn’t a “set it and forget it” deal; it’s a partnership.
Let’s get real about common mistakes I see. Number one: operators skip the pre-check. They hit “run” without checking the gas pressure, wire feed speed, or path for obstructions. I make them do a pre-check list every single time, and sign it – no list, no start. Number two: they don’t update the program when the metal changes. If a batch of steel is ½ inch thicker than last week, the program needs a travel speed adjustment. I have a rule: if the metal isn’t the same as the last run, you re-program the path for that section. Number three: they forget to maintain the robot. A lot of shops see the robot as “set it and weld” and skip cleaning the torch or lubricating the gantry rails. I do a 1-hour maintenance training on day two, show them how to change the contact tip, clean the lens, and check the rails – small things that add up to longer robot life.
Wait, let’s mention what we do for bigger teams. If you have 10 or more operators, I recommend a “train the trainer” model. We pick one or two people from your team, train them on all the ins and outs, and then they train the rest. That way, when I’m not around, you’ve got someone in-house who can fix small issues without calling us. We give a free train-the-trainer session with every robot order over 5 units, which is a steal. I had a shop in Ohio do this, and their in-house trainer is now the go-to person for all their robot questions – saves them so much time and money.
At the end of the day, training is about building confidence, not just checking boxes. I’ve had operators who swore they’d never use a robot go from hating the teach pendant to loving it because it makes their job easier – no more 8-hour days holding a torch, no more hand fatigue from welding thick metal. Last year, a guy I trained in Atlanta told me he went from making $18 an hour welding manually to $22 an hour running the robot, because his output went up 30%. That’s the win we’re all after: making your team’s job better and your shop more efficient.
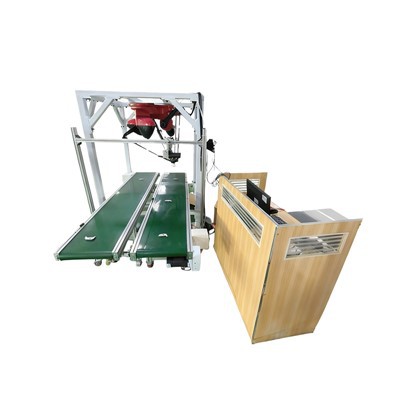
If you’re reading this and you’ve got a gantry welding robot that’s underperforming, or you’re thinking about buying one and worried about training, hit me up. We don’t do rigid one-size-fits-all training plans, we work with your team to make sure they feel comfortable, safe, and actually good at running the robot. No boring lectures, no confusing jargon, just real-world stuff that gets results.
Nail Gun Robot References:
- American Welding Society (AWS). Robotic Welding Safety Guidelines, 2022.
- FANUC Robotics. Gantry Welding Operator Training Best Practices, 2021.
- OSHA. Safe Operation of Industrial Robots in Manufacturing, 2023.
Dongguan Chuanglida Intelligent Equipments Co., Ltd.
Address: Room 201, Building 2, No. 61, Shachang 1st Road, Dalang Town, Dongguan City, Guangdong Province
E-mail: haoguangli001@outlook.com
WebSite: https://www.boruntestech.com/
